




- Machine de traitement d'huile de transformateur sous vide à deux étages
- Machine de traitement d'huile de transformateur sous vide montée sur remorque
- purificateur d'huile de lubrification (turbine / hydraulique)
- purificateur d'huile de transformateur sous vide à un étage
- système de purification d'huile de déshydratation sous vide
- purificateur d'huile isolante
- filtre à huile portable
- purificateur d'huile de type coalescent
- séparateur d'huile centrifuge à disque
- système de filtration d'huile diesel (carburant)
- presse filtre machine
- unité de pompe à vide
- système de purification de séchage à l'air
- équipements de test
- station de traitement de gaz sf6
- Cuves de filtration & accessoires
Acore Filtration Co. Ltd.
- Tél. : +86 132 06063693
- Email : sales@acorefiltration.com
- mobile et WhatsApp : +8613206063693
- Télécopieur : +86 23 8132 4618
- Ajouter : No.2, Jianhe Road, Banan District, Chongqing, China
Cas
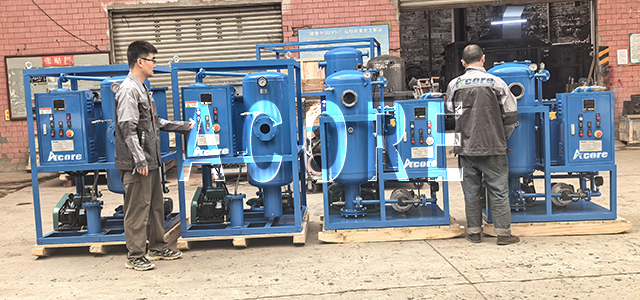
Four sets of HFR10 Phosphate Ester Fire-resistant Oil Purifier Sales to Pakistan
September 28,2026.
In modern industrial production systems,
hydraulic systems are the core power components of various heavy machinery,
precision equipment, and automated production lines, widely used in mechanical
manufacturing, metallurgy and mining, chemical production, and many other
fields. Hydraulic oil or Phosphate Ester oil, as the
"lifeblood" of the hydraulic system, plays a crucial role in
lubrication, sealing, transmission, and cooling. The cleanliness and quality of
the oil directly determine the operating condition of the entire equipment.
During long-term, high-load operation in industrial production, hydraulic oil
is prone to contamination by water, air, metal debris, and dust particles,
gradually leading to deterioration, emulsification, viscosity reduction, and
other problems, which are major causes of equipment jamming, leakage, abnormal
noise, and shutdown failures. A Vacuum Hydraulic Oil Purifier for hydraulic
oil, as a specialized oil filter machine, is key to ensuring oil quality,
reducing equipment failure rates, and maintaining stable production line
operation.
In industrial production, most hydraulic equipment failures originate from oil
contamination. Long-term operation produces metal wear debris, and workshop
dust and moisture may seep into the oil via equipment gaps. At the same time,
hydraulic oil can mix with air and generate oxidation products during
high-pressure circulation. Contaminated hydraulic oil greatly reduces
lubrication performance and accelerates wear on precision components like
hydraulic pumps, control valves, and cylinders, causing valve sticking, oil
circuit blockages, and unstable pressure. Minor contamination can reduce
operational precision and production efficiency, while severe contamination can
lead to sudden equipment shutdowns and component corrosion, disrupting
production schedules and increasing costly repairs and part replacements,
making it a hidden pain point in industrial production.
The core value of a Phosphate Ester Fire-resistant Oil Purifier lies in
addressing oil contamination at the source, laying a solid foundation for
stable equipment operation. Unlike ordinary simple filtration equipment, it
relies on a purification method combining vacuum separation and precision
filtration to remove various contaminants from hydraulic oil. The device
efficiently separates free water, emulsified water, and dissolved gases from
the oil, solving issues of milky or foaming oil and restoring the oil's
original physical and chemical properties. At the same time, it precisely
filters out particles, metal debris, and oxidation deposits, keeping hydraulic
oil consistently clean and stable, perfectly suited for long-term continuous
operation of industrial equipment.
Stable oil quality is key to reducing equipment failure rates. Hydraulic oil
purified with a vacuum Phosphate Ester Fire-resistant Oil Purifier restores lubrication, transmission, and cooling performance, effectively
reducing internal friction in the hydraulic system and avoiding common issues
like valve sticking, oil circuit blockage, and pressure imbalance. Long-term
use can significantly reduce the occurrence of oil leaks, abnormal noise, and
power shortages, preventing sudden downtime. Numerous industrial applications
have proven that regularly vacuum-purifying hydraulic oil can greatly reduce
hydraulic system failures, extend the service life of core components like oil
pumps and hydraulic valves, and keep equipment operating efficiently and
stably.
Besides reducing failure risks, a vacuum Hydraulic Oil Filter Machine helps
companies drastically cut production and maintenance costs. In traditional
production, slightly contaminated oil is often replaced with new oil, causing
wastage and incurring ongoing waste oil disposal costs. A vacuum hydraulic oil
purifier enables the recycling and regeneration of hydraulic oil, reducing the
need for frequent oil changes and lowering procurement costs. Meanwhile, fewer
equipment failures, reduced parts wear, and shorter downtime prevent production
losses, improving overall production line efficiency and helping businesses cut
costs and increase efficiency.
In large-scale, continuous industrial production, equipment stability ensures productivity. Though a Phosphate Ester Fire-resistant Hydraulic Oil Purifier may seem like an auxiliary purification device, it plays a crucial role in protecting the entire hydraulic system and ensuring uninterrupted production. By addressing oil contamination at its source, the hydraulic oil filter machine reduces equipment failure rates in a cost-effective and efficient manner, prolongs equipment life, and serves as an essential maintenance tool in modern industrial production. It's also a critical guarantee for stable production and improved efficiency in enterprises.


 +8613206063693
 Rufus Huang
 sales@acorefiltration.com
 +8613206063693
 +86 23 8132 4618
